2026 Top Types of Stick Welding Sticks for Buyers
Choosing the right Stick Welding Sticks can change how easily an arc starts, how the bead forms, and how much cleanup a job needs. Yet no single electrode works best for every welder or workpiece. A rod that performs well on a rusty outdoor repair may be a poor match for a clean, thin steel panel. Small details matter.
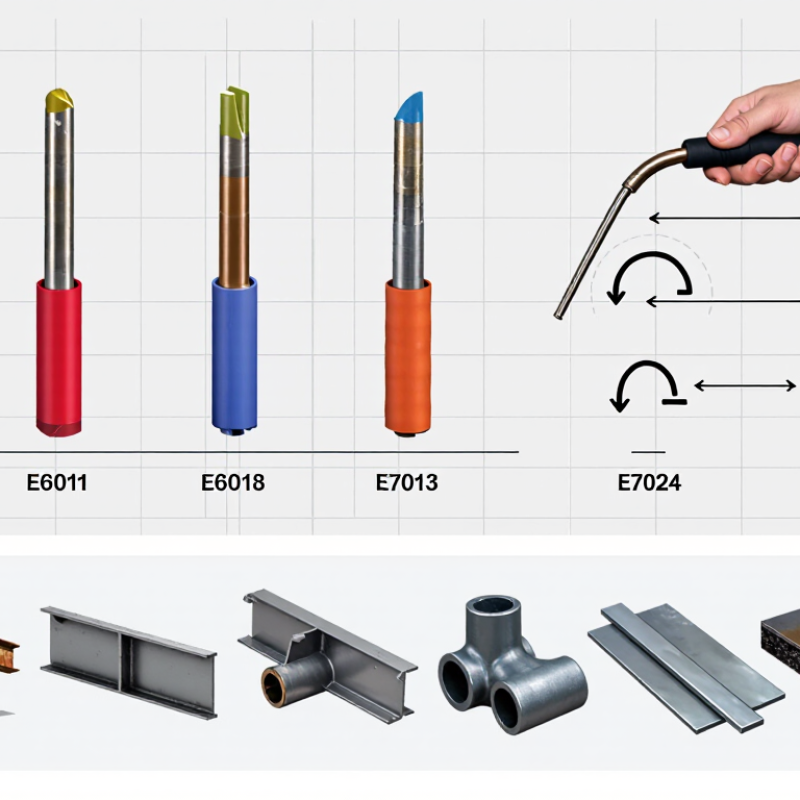
This 2026 buyer’s guide introduces common choices, including E6010, E6011, E6013, E7018, and E7024. Their coatings and intended uses differ. Cellulose-coated rods are often selected for digging arcs and field work, while rutile rods can offer a smoother feel for general tasks. Low-hydrogen electrodes require closer attention to storage and handling. E7018 is not automatically the best answer.
We’ll compare typical applications, arc behavior, penetration, slag removal, and practical buying considerations. We’ll also explain why electrode diameter, base-metal thickness, welding position, power source, and polarity should guide a purchase. Check the package and manufacturer’s data sheet for the exact requirements. Those specifics can vary by product.
The labels help, but they do not tell the whole story. Your first pass may still look rough. That is useful feedback, not a verdict. A sensible choice starts with the job in front of you, then balances performance, ease of use, and cost.
What Stick Welding Electrodes Are and How They Work
2026 Top Types of Stick Welding Sticks for Buyers
What Stick Welding Electrodes Are and How They Work
A stick welding electrode is a metal rod covered with a flux coating. The rod carries welding current and melts into the joint as the arc heats the workpiece. Meanwhile, the coating produces shielding gases and forms slag over the cooling weld. This helps protect the molten metal from contamination. The electrode is consumed during welding, so the welder gradually feeds it toward the joint. Simple in principle, but the arc takes practice to control.
Electrodes differ in coating, strength, and recommended operating conditions. Some suit general-purpose repairs, while others are designed for particular steel types or welding positions. Check the electrode classification and the machine’s instructions before choosing current or polarity; requirements vary. In practice, the weld puddle may feel less predictable on rusty or uneven material. Clean preparation helps, though it cannot fix every setup problem.
Tips: Keep electrodes dry and store them as their packaging directs. Use a steady travel speed, and watch the small pool of molten metal rather than the bright arc alone. Remove slag between passes with suitable tools, then inspect the bead for gaps or trapped debris. Keep it simple. Even experienced welders sometimes need to adjust their technique when the joint or material changes.
