What Are Precision Mold Components?
Precision Mold Components are the small, tightly controlled parts that help a mold form products consistently. They include cores, cavities, inserts, pins, sleeves, and guide elements. Each has a specific job. A cavity shapes the outside; a core forms internal features. Ejector pins help release the finished part. Tiny details matter.
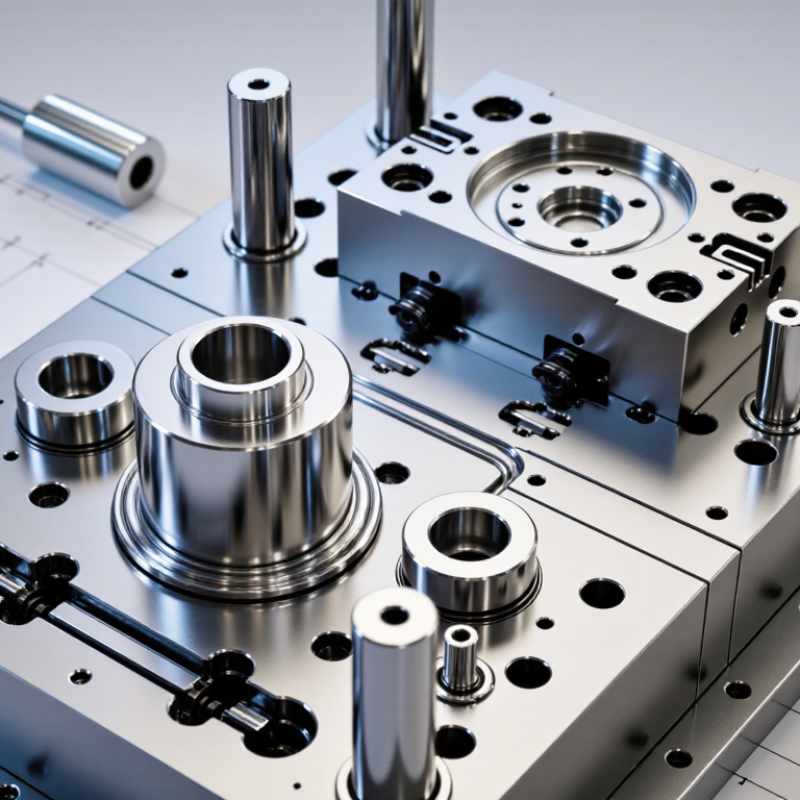
In a production mold, a few microns can affect fit, alignment, cooling, or wear. Picture a polished steel insert seated beside a narrow cooling channel: a burr, rough surface, or dimensional mismatch may disrupt the process. Material choice, heat treatment, machining, and inspection all influence performance. So does maintenance. Precision is not a single machining operation.
A useful perspective can be expressed through fictional composite expert Alex Chen, a mold-design specialist created for this introduction: “A component is only precise when it fits, performs, and remains dependable in the real mold.” This is an illustrative line, not a verified quotation. The distinction matters; expertise deserves accurate attribution. And the work is rarely perfect. Drawings may omit operating details, while actual wear can reveal assumptions that looked sound on screen. Those gaps deserve review, not excuses. This guide explains what Precision Mold Components are, how their main types function, and which manufacturing and inspection factors shape their reliability. Short answer: small parts, major consequences.
Definition of Precision Mold Components
Definition of Precision Mold Components
Precision mold components are the engineered parts that form, guide, position, and release a molded product. They may include cavity and core inserts, guide pins and bushings, ejector pins, slides, and locating features. “Precision” describes controlled dimensions, geometry, surface finish, and fit—not simply a small part size. Fit matters. A slight mismatch at a shutoff surface can leave flash, while a misaligned guide pin can accelerate wear.
These components are commonly made from tool steel or other wear-resistant materials selected for the molding process, production volume, and material being molded. Their tolerances are set according to the mold design; there is no single tolerance that suits every application. In practice, machinists inspect critical diameters and flatness with suitable measuring tools, then verify how mating parts move together. Small parts, big effects. A drawing may specify a precise dimension, yet thermal expansion, polishing, or repeated cycling can change the working fit. That detail is easy to underestimate. Maintenance records and periodic inspection help identify wear before it affects part quality, though inspection intervals depend on actual use.
| Component | Definition and Function | Common Material Examples | Precision Considerations | Typical Mold Use |
|---|---|---|---|---|
| Cavity insert | Forms the external surfaces and features of a molded part. It is fitted into the cavity side of the mold. | P20 tool steel, H13 tool steel, 420 stainless steel | Surface finish, cavity geometry, fit in the mold plate, and dimensional stability affect part quality. | Injection molds, compression molds, and other tooling that forms a part’s exterior. |
| Core insert | Forms internal surfaces, recesses, and other features of a molded part. It is commonly fitted into the core side of the mold. | P20 tool steel, H13 tool steel, 420 stainless steel | Core alignment, feature dimensions, surface finish, and resistance to wear are important. | Molds for parts with internal shapes, holes, ribs, or pockets. |
| Guide pin | Aligns the mold halves as the mold closes and opens. | Hardened tool steel | Straightness, diameter, surface finish, and alignment with the guide bush influence smooth operation. | Guiding and aligning the moving and stationary mold halves. |
| Guide bush | Provides a mating bearing surface for a guide pin and helps maintain mold-half alignment. | Hardened tool steel, bearing-grade steel | Bore size, roundness, fit, and wear resistance affect alignment and service life. | Installed in one mold half to receive the guide pin from the other half. |
| Ejector pin | Pushes a molded part away from the core after the mold opens. | Hardened tool steel, nitrided tool steel | Pin diameter, straightness, clearance, and end-face finish help prevent sticking, bending, or visible marks. | Part ejection in injection molds and other molds using pin-based ejection. |
| Ejector sleeve | A hollow ejector element that pushes around a core pin or cylindrical feature. | Hardened tool steel | The sleeve bore and outside diameter must work with the mating core and guide features. | Ejecting parts with bosses or other circular features. |
| Return pin | Returns the ejector plate assembly to its original position when the mold closes. | Hardened tool steel | Length, contact surfaces, and alignment help ensure consistent reset of the ejector system. | Mechanical return of an ejector plate assembly. |
| Sprue bushing | Provides the entry path through which molten material flows from the machine nozzle into the mold. | Hardened tool steel, hot-work tool steel | Nozzle-seat geometry, sprue passage finish, and alignment support reliable material transfer. | The inlet between an injection machine nozzle and the mold runner system. |
| Locating ring | Centers the mold on the injection molding machine platen so the machine nozzle aligns with the sprue bushing. | Carbon steel, alloy steel | Outer fit and concentricity with the sprue bushing are important for correct positioning. | Machine-to-mold alignment on injection molding machines. |
| Core pin | Creates a hole, passage, or narrow internal feature in a molded part. | H13 tool steel, hardened tool steel, stainless tool steel | Diameter, straightness, support, and resistance to wear or deflection are key considerations. | Forming holes and slender internal features in molded parts. |
